Category Archives: Business

Green Innovation Lag

It is not unusual for a long time to elapse between an initial customer inquiry and when commercial quantities of product are loaded on the truck and driven out the gate. I have seen it happen over 1 to 10 years, with 3 years being quite common. The chemical industry is not like the semiconductor business. The paradigm shift period seems much longer. In fact, any given chemical processing technology can last for a large part of a career or more. The last big chemical paradigm shift I have noticed is high throughput experimentation (HTE).  Maybe others have a more recent example.

Green chemistry is considered by many to be a new frontier of opportunity. To its detriment, many of us are unsure of what green chemistry really is and how to implement it in manufacturing. Realistically, for green chemistry to find wide acceptance, it needs to turn a profit or offer some kind of concrete advantage. Pollution avoidance is too abstract. For any new method or technology, there must be a payoff.

It seems simple. Reduce VOC emissions by using aqueous solvent compositions. Increase atom efficiency in transformations. Minimize persistant pollutants, organic or metal. Increase space yields, reduce consumables.  Green chemistry is not so easily demonstrated to the public and it may not be in the public domain. Your green technology may be proprietary, so the ballyhoo factor will collapse to zero. The processor may have to labor down the green path in silence.   

A process changeover to a green process may require many people in several companies to align to the change like compass needles to the north pole. A chemical process change must offer some kind of improvement that, by consensus, is meritorious. There is a good chance that the change will require notification of the customer and possibly even their permission. Customers often want a price concession when there is a process change so they can capture some of the value, so this may mean reduced sales volume and profits for the processor.

The customer may require that the proposed process change will be cause for a new validation of their customers product, in which case, the final user will also have to perform a validation.   In all likelihood, you are proposing a green change to a process that previously offered no problem to the downstream users.

Obviously, the time for green process implementation is at the very beginning of process development. The development chemist must have an existing toolbag of techniques, transformations, and reagents to choose from to go forward with implementation. The best way to get to this point is with curriculum change at the university level. Chemists need to have green chemistry awareness from the beginning of their training. Converting souls when they are already within industry is the hard way to do it.

Microscale labs in the undergrad experience maybe green for the university, but it is hard to see how it translates to the implementation of green technology in industry. The green revolution must come from textbooks that use green transformations in chemistry and engineering coursework. It must come from professors who weave it into their lectures and provide examples of such transformations and practices in the lab experience.

Chemists and engineers from such backgrounds must move into industry and become group leaders and managers. Only at this point will green chemistry become “normal” and expected.

Shermer’s “Mind of the Market”

Google has been posting a series of interesting talks by contemporary authors. This talk is by Michael Shermer, author of Mind of the Market, and editor of the popular magazine Skeptic. It is a lengthy 53 minute video, but I would highly recommend it. I think Shermer has a good grasp on the anthropology of our present world.

This is off-topic, but useful. This link gives a bunch of really good hints on how to save money for your start-up company.

Incident Attenuation in Chemical Plant Design

If you work in a location that handles or processes hazardous materials, eventually you have to come to grips with the matter of risk and accidents. It is possible to design procedures that prevent certain kinds of accidents and casualties.  It is possible to install devices and automated contrivances that can eliminate specific failures and the resulting cascade of multistage calamities that might follow.

Over time and with plenty of thought, a chemical plant can be fool-proofed to a large extent. But in the end, residual margins of safety depend on the man-machine interface. People have to undergo recurrent training and certain staff must be assigned to specialize in safety.

All devices have a failure rate. The rate may be small or large. A device may fail safely or not. Most chemical plants are, to a large extent, hand built. They are fabricated by skilled tradesmen who connect pre-fabricated parts to one-of-a-kind assemblies built on-site. In this way, expertise is captured from the plant designers, contractors, and the manufacturers of the installed equipment.  In the end though, it is up to the designers to assure that there is compatibility and some margin of overdesign in the finished facility.

While it is possible to assemble a facility from the very best equipment, the fascinating question of design for the attenuation of accident propagation is not often discussed, at least openly.  Accidents can usually be reduced to a few characteristic phases. They are initiation, propagation, and termination. 

An incident begins with an initiating event. Some release of hazardous energy is presented to the surroundings that may begin a propagation of undesired events. Events can propagate in series or parallel chains.  Hazardous energy can be electrical, chemical, or mechanical. The initiation is the tipping of a domino as a triggering event that causes the release of other hazardous conditions to ensue. Eventually, the propagation of the hazardous energy release is suppressed, extinguished, or simply exhausted in the termination phase.

One of the best ways of learning about the phenomenon of accidents is reading about them. A website worth visiting is the US Chemical and Hazard Investigation Board. It is useful for chemists and engineers to study the anlyses of the CSB and gain useful insight into the dynamics of chemical plant accidents.

It is possible to configure a chemical plant in such a manner as to attenuate the propagation of hazardous energy during an incident. In general, a large distance between reservoirs of potential energy is the easiest solution. Explosives manufacturers have known this for a long time. One well known German manufacturer of energetic materials has a manufacturing site spread over a large rural area and has built in bunkers with berms and trees to attenuate the propagation of shockwaves and allow flying fragments to land safely in an uninhabited area.  Fortunately, not many manufacturers have processes and products requiring this kind of design consideration.

Situations of “ordinary” risk magnitude do require some thought, however. Consider the storage of drums of flammable materials. Most companies that handle palletized drums of flammable liquids meet the minimal fire and insurance codes for the handling of these materials.

But consider this. What if a forklift driver spears a drum of solvent with his lift, and then in a panic, backs up and pulls the fork out of the drum resulting in a spill? At this point, policy and regulations are irrelevant. The only question is this-  Where does the liquid and the potential fire go?

Indoor storage of flammable materials requires fire suppression. Fire suppression is not the same as fire extinguishment. It is about knocking down the fire to a manageable level for emergency egress, to suppress the spread of the fire, and for firefighters to make some kind of attempt to extinguish the blaze. This is routine firefighter stuff.

What is less than routine, however, is the issue of BLEVE’s. I have written on this phenomenon previously.  Fire suppression is one thing, but BLEVE’s – Boiling Liquid Expanding Vapor Explosions- are quite another matter to deal with.

This is where a well designed facility with passive architectural features to attenuate the spread of hazardous energy can be helpful. An indoor BLEVE is virtually assured to accelerate the pace of a disaster.  So, in the planning phase of a plant, it is important to consider how energy release during an accident may propagate.  Drummed flammable liquids should be isolated from work areas and egress paths. This is pretty obvious to initial designers, but not necessarily years down the road during an expansion.

Consideration should be given to the anticipated direction in which energy is released. Where possible, energy should be released away from populated areas and away from major capital equipment. A fire in a materials storage area shouldn’t lead to an extended plant shutdown due to damaged process equipment. Segregation is key to plant safety and business viability.

Smoke is a potential killer and there are architectural tricks that can add provide slightly greater safety margins. Ceilings designed to collect and channel smoke out of the space could reduce the likelihood of suffocation of stranded workers and suppress the chances of a flashover. Smoke curtains properly placed can channel smoke away from hallways and the resulting spread.

Another concern is the fate of spilled flammable liquids in a storage area. Where should the spill go? Should the spill be concentrated in a small space or channeled to another space where a fire can burn with lower negative consequence? Nobody likes to pay for an overengineered warehouse, but fire resistant partitions in a solvent storage area can go a long way toward the isolation of a fire and attenuation of a larger scale calamity.

One major plant accident I am familiar with has a number of attributes that other operators would do well to consider.  A 750 gallon reactor explosion resulted in the complete fragmentation of the vessel.  A few pieces ejected from the hole in the roof were found lodged in the walls of neighboring structures off-site.  Fortunately, this reactor was in an enclosed space with no other reactors or stored hazardous materials. In one way, this accident was isolated due to passive attributes. However, the building space was interconnected to other spaces by a series of adjacent rooms and hallways. While fragmentation and fire damage were contained due to the happy fortune of isolation, the shockwave was able to follow all of the connected and enclosed pathways.  The connected pathways were a convenience to the workers, but this feature channeled a pressure wave throughout the entire facility, lifting the roof enough to damage large -remote- sections of it as well as badly damaging overhead doors and windows throughout the facility.

Take home lessons? 1) Leave open space walkways between production and storage buildings and the rest of the facility. Collateral damage is likely to be suppressed with this cheap, passive feature. 2) isolate and dedicate certain vessels to hazardous operations. 3) Store hazardous materials well away from processing areas. Storage and processing have their own hazards and a disaster in one area should not be allowed to propagate to the other.

The matter of flammable solvent storage and accident attenuation is only partially solved with enclosed flammable materials lockers. It seems to me that some research should be done to advance the level of best practices in this area.
Sigh

What a horrible week.  >>>>>>***Sarcastic comment stricken from the record***<<<<<  Things have gotten too Machiavellian.

Let’s talk about sunshine and daisies instead:  Some things about Th’ Gaussling that may not be widely known- I wear a Mickey Mouse watch, even on business trips, and I am a daily user of a pocket protector. My current pocket protector is emblazoned with the logo “Buca di Beppo”.  I’m considering having some Lamentations on Chemistry pocket protectors printed up for distribution from this site.

Email Etiquette- Going Nuclear

A pet peeve I have with my some fellow adult co-workers is their bad habit of excessive cc’ing people on emails. The most pernicious version of this is an email where a list of grievances is sent around with the conspicuous presence of some upper level manager carbon copied, or worse, blind copied.

This habit is a transparent kind of tattle-tale leverage used in the art of persuasion. Once someone has “publically” complained to upper level folks, everyone else has no choice but to opt for CYA.  It is like a nulcear weapon- once released, it knocks everyone down. I refer to these situations as “going nuclear”.

People feel that they have to respond in kind.  One email escalates to many. Soon, there is a flurry of emails clogging the inboxes of those trapped in this fetid tidal pool. Eventually, the tempest dies down leaving the boss wondering about the judgement and temperament of the staff. 

The worst kind of cc is the bc, or blind copy. This method is favored by practitioners of the dark arts. It is a truly reprehensible practice and people who do it should be hunted down like the rabid  curs they are and tarred and feathered. Neutered, maybe.

Ab Initio Chemical Plant Design

So, dear reader. If you were going to design a general/multi-purpose chemical plant capable of doing a wide variety of chemical transformations, what kind of features would you install now that you’ve had some experience in the field? No high pressure vessels, just ambient to 80 or 100 psi. I’m talking about a plant with 50 to 2000 gallon reactors- say, 8 of them. What kind of configurations would be desirable starting from the ground up?

No GMP capacity- too bloody expensive. We don’t want to do API’s.  No gas phase chemistry. No scary oxidation chemistry or energetic materials.  Just the kind of garden variety specialty organic or inorganic compounds and transformations that you might find in the Aldrich catalog.  Synthons, reagents, etc.

One interesting thing to ponder are possibilities with the use of passive architectural features to attenuate the propagation of upset or emergency conditions. 

PGM Prices Remain Strong

The Platinum Group Metals (PGM’s) continue to trend upwards.  Last friday 0n the EIB rhodium opened at US$9,050.00/toz. Rh remains in strong technical demand and prices are propped by a great many overlapping factors. Uncertainties in the mining business in South Africa buoy uncertainty among investors. Recent electrical distribution shortfalls and blackouts have interrupted production as have mine floods, labor disputes, and a shortage of experienced miners and managers.

Automotive pollution catalytic converters dominate the demand for platinum and rhodium. As demand for Pt and Rh continues to grow, look for companies to switch to palladium in key applications.  Russia holds a strong position in Pd inventories. As demand for Pd rises, look for Russia to exercise its muscle.

As Au and Pt prices continue to climb, look for jewelry demand for these metals to taper off.  Asian demand for these metals is substantial. Eventually, jewelry prices will temper demand for gold and platinum.  Meanwhile, interest grows in North American PGM resources.

Password Blues

Our IT guy has been hounding us to make better choices for login passwords into the company information system. More characters, digits, and the use of mixed case is recommended. Like many people, I have accounts in diverse systems that are not connected. Not every system gives me a choice of login names and passwords.  Eventually one ends up with a variety of codewords that one has to keep straight. Soon it becomes a little burdensome.

There is a website that purports to provide random character strings. It is Random.org.  The operator of the site is a lecturer in computer science at Trinity College and uses atmospheric noise from a group of radios to capture random events that are somehow translated into character strings.

If you need strings of random digits, there is von Neumann’s middle square method. It can be done on a calculator. While it is hard to guarantee that there isn’t some kind of periodicity, von Neumann felt this method suited his needs.

I wonder to what extent the shaky state of internet security depends on the structure and prevalence of Microsoft code?  I have no idea.

Literature Swim. The Guo-Liu Catalyst.

Guo & Liu Catalyst

The literature train station is overflowing with diverse catalysts for the large variety of coupling reactions out there, as is the patent literature. Parties scramble to get window seats on the IP Express, the high speed non-stop to that Golden City on the Hill. 

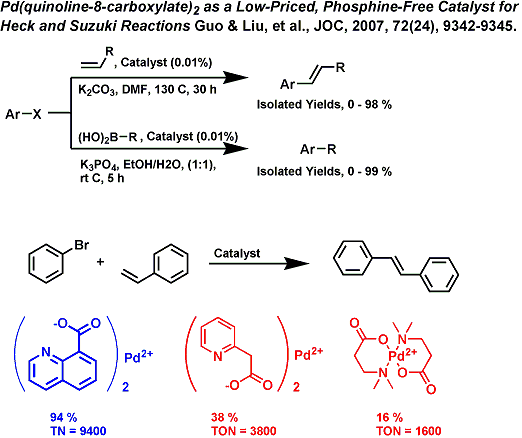
A recent JOC article disclosing an inexpensive catalyst system that struck me as interesting.  The article by Guo and Liu emphasizes economy and so discloses a phosphorus-free bidentate ligand system that affords Heck and Suzuki-type coupled products.  There are pluses and minuses to this system, as is the case for most catalysts.

On the plus side with the Heck and Suzuki reactions, both activated and deactivated aryls gave decent yields. On the minus side, the Heck coupling reaction is a bit slow. A fair amount of energy input was needed- 130 C in DMF over 30 hours. On the Suzuki side, most reported reactions resulted in good yields, except for the aryl chlorides. The relative inertness of chlorides is not particularly unusual, but it may cause this catalyst to be passed over in some applications where the less atom-efficient bromides and iodides have been targeted for replacement.

Finally, the apparent requirement of DMF is rarely happy news. Regardless, I have no doubt that this catalyst will find its way into the future literature and many clever applications will be revealed.  As of this writing, I was unable to find a US patent by inventors Guo and Liu claiming this technology. Since there is a 1 year limit on the filing of a patent application following disclosure, this technology could be in patent prosecution at present. Or not. Wouldn’t it be a happy thing for it to be in the public domain?

Economic Katrina

I’m reluctant to sound alarmed, but with the apparent shape of an impending economic Katrina moving over North America, it is getting harder to grant the benefit of the doubt. The dollar is sinking, exposing this import-heavy nation of ours to price increases in nearly every sector. The petroleum resources that energize global production and grease all economic skids is generating considerable doubt and turmoil in financial circles.

Oil production is flat in many key regions but the demand for consumer goods by the global middle class is expanding.  Our television-enchanted population, brains scrambled to numbness by chronic exposure to American Idol, are seeing only what the media powerbrokers want us to see. The eternal message that comes from TV is spend, spend, spend. 

The popular economic indicator is the stock market. The DJIA up- good. The DJIA down- bad. It is a sort of pallative. We’re lulled into a false comfort zone by the meta-stability of todays stockmarket.  Other dots are beginning to line up into a harmonic convergence, however.

Yesterday, as a humorous conversation starter, I asked a senior colleague well placed in the petroleum industry this question- “when will crude oil hit $150/bbl?”.  His reply surprised me. He estimated that it would happen this summer. Later, tempering his answer somewhat, he suggested that it would be more like $130/bbl, and mostly on the strength of nervousness in the market. He added that at present, crude oil stocks in the USA were in ample supply. 

The extended weakness in the dollar seems to favor American exporters and disfavors import consumers. Hmmm.  Does gov’t inaction on the weakness of the dollar amount to bias for corporate constituents and neglect of unincorporated citizens? Curious.

Advice- payoff as much debt as possible. Insulate your house. Get rid of that gas guzzler. Accumulate greater savings. A lot of the soon-to-be-unemployed are going to face higher higher gasoline prices for their commute to the new job at the auto salvage yard. And when they get back to their trailer at night, the thermostat will be set low due to higher heating costs. Beans and weenies, Mac-n-Cheese. Bon apetite!